The short answer: a bent prong is a mechanical event, not a plating event. Plating is a surface layer measured in microns — 2.5 microns of gold is the legal floor for vermeil under 16 CFR 23.4 — and that layer carries no structural load. It can lift, blister, discolour or wear through, but it cannot bend metal. When a ring leaves a silver polishing machine with a prong curled over the stone, the cause is the polishing action plus the metal it acted on: a thin wall at the bend, an internal casting pore, or a weak joint below the seat. The two-minute test is a witness test. Find where the bend sits relative to the seat, loupe the deformation at 10x, and check whether the gold layer is still intact across it. Deformed metal with intact plating means the plating is a bystander. Porous or paper-thin metal at the bend means the setting is the flaw.
Why a Polishing Machine Bends Prongs but Does Not Cause Plating Flaws
Most explanations stop at “it is snagging, not chemistry.” That is right and still not operational — you are left deciding whether to blame your finisher, your supplier or the design.
What actually happens inside a barrel, bowl or pin finisher
A polishing machine — rotary barrel, vibratory bowl or pin finisher — moves dozens of pieces against media for minutes to hours. The highest points on a ring are the prong tips and the stone table. Any prong that hooks a piece of media, a neighbouring ring or a chain gets a lever arm around the stone seat. The force arrives as a pull, not a squeeze, and it concentrates at the thinnest section of the prong wall. Sterling silver moves before it breaks, because what makes a piece easy to polish also makes it easy to deform.
Why a plating flaw is a different failure family
Plating defects are surface-and-adhesion events: blistering where the substrate was not perfectly clean, patchy colour from a contaminated bath, wear-through on high points after months of abrasion, flaking at edges when prep before the tank was weak. In every case the metal underneath keeps its shape. That is the distinction — plating can fail without mechanical movement, and metal can move without any plating failure.
Regulation frames it the same way. Vermeil is defined by composition, coating durability and thickness: a sterling silver base, gold or gold alloy of at least 10 karat fineness, a coating of “reasonable durability”, and a minimum thickness equivalent to 2.5 microns of fine gold (16 CFR 23.4). That durability language is about the plating staying put on the surface; nothing in the definition speaks to mechanical strength, prongs or settings, because a micron-scale layer has no structural role to speak of. The silver-content rule runs the same kind of check — it governs how a piece may be described, down to requiring that silver-plated representations rest on a plating or coating of silver “of reasonable durability” across all significant surfaces (16 CFR 23.5), not how much load a prong can carry.
Three Setting and Casting Causes That Get Blamed on the Plating
1. Prong walls that are too thin at the bend point
What matters is the cross-section through the prong wall, not the prong’s apparent width from above. A tip that looks generous in a front-facing product photo can taper to a wafer where it meets the seat.
A working bench benchmark for triage, and one you can write into your own drawing spec: on a prong holding a 6.5 mm round, aim for a tip section roughly 0.8–1.1 mm across and a wall at the base of the tip no thinner than about 0.5 mm; under roughly 0.4 mm at the bend point, treat the piece as light-duty. That is a shop-floor rule of thumb, not a published standard, and it does not replace an agreed acceptance criterion — but it sorts a complaint into “handling damage” or “under-built design” in under a minute.
2. Casting porosity: the prong that was hollow from the start
Casting defects hide inside the metal, which is why they survive bench inspection and resurface later as complaints. Gas porosity — trapped air or moisture in the mould — reads as round, smooth-walled voids: small dark pits at 10x. Shrinkage porosity is lacy, spongy and connected, and it appears at the thick-to-thin transition, which on a ring means the prong-to-seat junction.
Either type turns a 1 mm prong into a shell. The read at 10x is straightforward: a dense casting shows a continuous highlight along a bent prong, while porosity scatters the light into points and shadows. If voids visible at the bend cover more than about a third of the cross-section, stop calling it handling damage.
3. Joints, seats and setting technique
If a prong is soldered to the head rather than cast with it, a cold or under-filled joint lets the prong lean instead of absorbing load; at 10x it shows a seam with a grey or porous line. Setting matters too: a prong burnished hard against the stone sits with preload and a lower profile, while a lightly burnished one stays proud, catches media sooner and bends sooner. Amara Jeweiry publishes 100% pull-tested settings — ask your supplier whether the test is per piece or per lot. The setting stage is covered in what a moissanite ring is, from the manufacturing side.
The Two-Minute Test, Step by Step
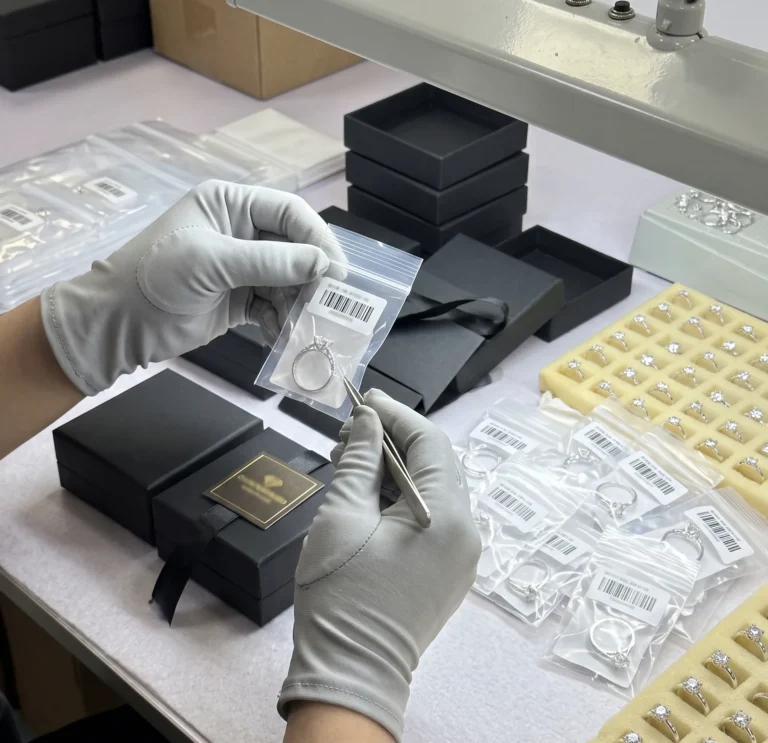
You need a 10x loupe, a raking light, and a phone with macro mode. Ninety seconds of the two minutes is looking; the rest is deciding.
- 0:00–0:30 — Locate the bend against the seat. Is the prong leaning away with its tip clear of the girdle, or folded tight while the stone sits firm? A prong bent where it meets the head, with no tool marks, took a snag load. Scuffs and bright scratches at the tip point to an abrasive hit.
- 0:30–1:00 — Read the plating as a witness. Follow the gold layer across the deformed prong. Bright, continuous plating says the coating survived the event, so no plating defect caused the bend. A single dull hairline on the outside of the curve says the coating cracked because the metal beneath yielded — again, mechanical. Blisters with the prong still straight point at a plating problem and a different claim.
- 1:00–1:45 — Loupe the deformation at 10x. Stretched and fibrous means the metal yielded cleanly. Dark round pits or a lacy sponge pattern mean the prong was porous. A crease inside the curve plus thinning outside is a classic thin-wall bend.
- 1:45–2:00 — Sort it into one bucket with the table below. Write the bucket on the ticket, and do not wash the piece first; the wrong cleaning cycle destroys the evidence.
| What you see at the bend | What it means | Next move |
|---|---|---|
| Plating bright and unbroken across a prong folded past 30 degrees | Mechanical snag during finishing | Re-tip and return; no spec change |
| Blisters or lifted patches with the metal still straight | Plating defect — prep or adhesion | Raise a plating claim; the bend is not the issue |
| One dull hairline on the outside of the curve only | Coating cracked because the metal yielded | Confirm mechanical cause; go to the decision line |
| Dark pits or lacy voids filling more than about a third of the visible section | Casting porosity | Hold the batch; raise the casting |
| Wall under roughly 0.4 mm at the bend on every piece of the style | Design is under-built | Thicken the prong or change the setting design |
What the Two-Minute Test Cannot Prove
It will not give you the alloy composition, tell you whether porosity runs deeper than the surface, or identify who applied the force. Nor will it verify plating thickness — a per-batch measurement or a lab job, not a loupe job. Send the piece out when the claim covers more than a handful of pieces or when a retail customer disputes liability in writing. The usual routes are XRF for surface composition, a metallographic cross-section for internal voids, and a plating-thickness measurement on a witness piece from the same batch. Photograph the piece first; a cross-section destroys it.
One limit worth stating plainly: the test does not prove intent. A supplier whose prongs are porous is not necessarily shipping junk knowingly — but a supplier who cannot describe the casting route is telling you something about the next batch.
Decision Line: Re-Tip, Reject the Batch, or Change the Design
- One piece, plating intact, no voids: handling damage. Re-tip by hand, touch up with hand polish only, return it. Do not re-tumble a plated piece — abrasive pastes thin the gold layer, as the care guide for moissanite rings and 925 silver explains.
- About 2% or more of a batch bending on the same style: a process or design signal, not bad luck. Ask your finisher for the route in writing — media type and size, loose versus bagged pieces, cycle time, and whether plated pieces run with steel media.
- Voids visible at 10x on any piece: hold the batch, inspect at your agreed sampling level (Amara Jeweiry publishes AQL 2.5 shipment inspection), and ask for a corrected casting run rather than rework.
- A style that fails twice in one season: change the design, not the paperwork. A heavier tip or a construction that hides the tips from media costs less than replacing stones all year.
What to Put in Writing Before the Next Production Run
Four lines in a spec sheet prevent most of these arguments: prong tip dimensions per stone size; whether prongs are cast with the head or soldered; the porosity standard and how it is inspected; and how tips are protected during finishing. Add a fifth if you sell vermeil: whether gold-plated pieces are tumbled separately from unplated silver, and what the supplier’s own vermeil thickness spec and per-batch spot checks look like. The vermeil and silver care section collects the background on how those layers wear.
FAQ
Can a plating flaw bend a prong?
No. A plated layer is microns thick and carries no load. A plating flaw can discolour, lift or wear through while the metal beneath holds its shape. If the prong moved, look for a mechanical cause: a snag, a thin wall or a pore.
My customer blames our polishing machine. Does that settle it?
The machine supplied the force; the piece supplied the resistance. Collect three details first: media type and size, how the load was mixed, and cycle time. If one style bent while the rest came out straight on the same machine and cycle, the variable is the piece — thin wall or porosity.
Can an ultrasonic cleaner bend prongs?
Ultrasonic energy is not the force that folds metal, but it can loosen a stone whose prong preload was already weak. The cleaning guide on this site treats ultrasonic as tolerable only for a fully bezel-set piece or a simple solitaire, and bans it on tennis and pavé lines. A stone that spins or clicks signals claw fatigue: re-set that piece.
Does moissanite make prong problems more likely?
No. Moissanite is lab-created silicon carbide at 9.25 on the Mohs scale. As the manufacturer’s explanation of the stone and its grading puts it, silicon carbide is chemically stable — it does not oxidize, cloud or fade — and it is the metal around the stone that ages first. A hard stone is not a strong setting: prong strength comes from the metal section and the joint, never from the stone.
Is a bent prong a warranty claim?
It depends where it bent. Amara Jeweiry publishes a 12-month anti-tarnish and stone-loss warranty and 100% pull-tested settings, and the setting half is what this argument turns on. A prong folded inside a buyer’s own polishing equipment is generally treated as buyer-side damage, so fix that boundary in writing before the first run and read the warranty wording as published.
Where This Fits in a Sourcing Program
ShenZhen Amara Jeweiry Co.,Ltd is an S925 sterling silver moissanite manufacturer in the Shuibei jewelry industrial belt, Luohu District, Shenzhen, operating since 2010, with 200+ silver moissanite designs, OEM/ODM and private-label programs, ISO 9001 certification, GRA and CMA certified stones, anti-tarnish plating, and 18K gold vermeil at 2.5 microns and above over recycled 925 silver. Minimum order is 30 pieces, mixed styles allowed. See the wholesale program, the certifications page, or the moissanite ring range if you want this test run against a production sample.